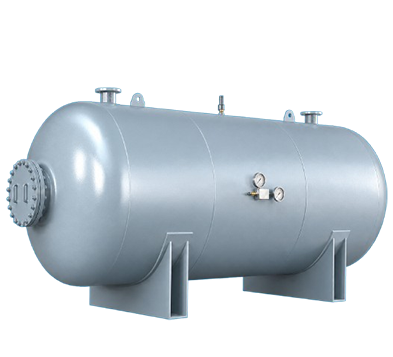
Air Receiver Tank for Cement Industry – Divya Engineers Private Limited
Cement manufacturing depends on reliable machinery, controlled material movement, and a steady compressed-air supply. From pneumatic conveying and packing machines to dust-control systems and automated valves, compressed air supports many critical operations. A properly designed Air Receiver Tank for Cement Industry helps maintain stable air pressure, stores reserve air, and improves the efficiency of the complete compressor system.
Divya Engineers Private Limited offers durable and application-focused compressed-air storage solutions for demanding industrial conditions. Our Air Receiver Tank for Cement Industry is designed to support continuous operations in dusty, high-load environments where equipment reliability and safety cannot be compromised. With the right capacity, pressure rating, and fabrication quality, an air receiver can help reduce compressor load and avoid production interruptions.
Why Is an Air Receiver Tank for Cement Industry Important?
Cement plants use compressed air for several functions, including pneumatic conveying, bag filling, silo aeration, actuator operation, cleaning, instrumentation, and control systems. These applications may require large volumes of air at different times. Without sufficient storage capacity, the compressor may cycle too frequently or struggle to meet sudden demand.
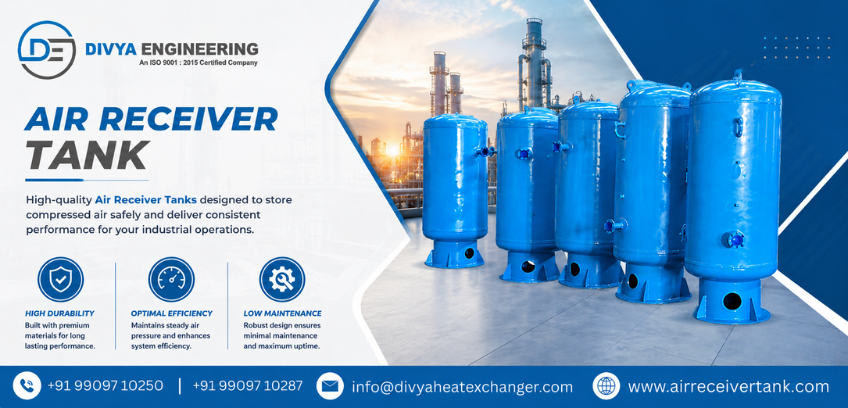
An Air Receiver Tank acts as a buffer between the compressor and the air-consuming equipment. It stores compressed air and releases it when demand rises. This helps maintain more consistent pressure, reduces unnecessary compressor starts and stops, and supports the smooth operation of pneumatic tools and process equipment.
In addition, the tank provides a cooling area for compressed air. As air cools, moisture may condense and settle at the bottom of the vessel. With proper draining, this helps reduce moisture entering the downstream air line. For cement plants, where dusty conditions are common, cleaner and drier air can support better performance of valves, filters, and automation systems.
Key Features of Our Air Receiver Tank for Cement Industry
Divya Engineers Private Limited manufactures tanks with features suitable for heavy-duty industrial service. Each tank can be selected based on compressor capacity, air-consumption pattern, available floor space, and required operating pressure.
Key features include:
Strong steel construction for industrial operating conditions
Suitable capacity options for varied cement plant applications
Vertical and horizontal tank designs
Robust inlet, outlet, drain, safety-valve, and gauge connections
Smooth internal space for compressed-air storage and moisture settling
Secure supports for stable installation
Custom nozzle locations and connection sizes, where required
Protective external coating options for improved durability
Pressure-testing and inspection support as per project requirements
A correctly sized Air Receiver Tank for Cement Industry can improve pressure stability during peak operations, particularly where multiple pneumatic systems work at the same time. It also provides a reserve that helps maintain continuity when air consumption suddenly increases.
Common Applications in Cement Plants
An Air Receiver Tank is a valuable component in many cement-industry processes. It can be connected to central compressed-air systems as well as dedicated compressor arrangements for specific plant sections.
Typical applications include pneumatic conveying of cement, fly ash, and other materials; air-operated valves; packing and bagging machines; dust-collection systems; silo aeration; instrument-air supply; clinker handling; maintenance workshops; and cleaning operations. It is also useful in systems where compressed air is needed intermittently but at a high flow rate.
The Air Receiver Tank for Cement Industry supports better management of these varying air demands. Instead of forcing the compressor to instantly match every demand spike, the receiver supplies stored air for short periods. This can improve equipment response and reduce strain on the air-generation system.
Quality Standards That Matter in Heavy-Duty Service
Cement plants create a challenging operating environment. Dust, vibration, long operating hours, and demanding production schedules require dependable equipment. Divya Engineers Private Limited focuses on fabrication quality so clients receive a strong and reliable air-storage solution.
As an experienced Air Receiver Tank for Cement Industry Manufacturer, we pay attention to suitable raw materials, plate thickness, welding quality, nozzle placement, structural strength, and finish. The vessel is fabricated to suit the required pressure and capacity specifications. Our production team follows careful fabrication and inspection practices to support consistent quality.
Quality is not only about the tank body. It also includes proper provision for connections, drainage, safety accessories, handling, installation, and maintenance access. A well-made receiver helps plant teams operate their compressed-air systems more confidently and efficiently over the long term.
Why Choose Divya Engineers Private Limited?
Choosing the right Air Receiver Tank for Cement Industry Supplier is important because every cement plant has different air-demand patterns and site conditions. A tank that is too small may not provide sufficient reserve air, while an improperly specified unit may not suit the pressure or layout of the system.
Divya Engineers Private Limited works with customers to understand their operating requirements before recommending a suitable solution. We aim to provide the Best Air Receiver Tank for Cement Industry through dependable fabrication, practical specifications, and responsive customer support.
Reasons to choose us include:
Durable construction for industrial use
Capacity and pressure options based on actual application needs
Customised fabrication support
Attention to weld quality and structural reliability
Suitable vertical or horizontal arrangements
Practical guidance for installation and use
Competitive commercial support for bulk and project requirements
Timely coordination from enquiry to dispatch
Our goal is to deliver a Top Air Receiver Tank for Cement Industry that contributes to safer, smoother, and more productive plant operations.
How to Select the Right Tank
Before you Buy Air Receiver Tank for Cement Industry, assess the compressor capacity, system pressure, peak air demand, duty cycle, and available installation area. Also consider whether the tank will be installed near the compressor room, a pneumatic conveying line, or a specific production section.
Vertical tanks can save floor space, while horizontal tanks may be more suitable where height is limited. The tank should include suitable connections for the inlet, outlet, pressure gauge, safety valve, and condensate drain. Regular draining is essential because accumulated water can affect system performance and may increase the risk of internal corrosion.
Discussing your requirement with a technical supplier can help you choose the right volume and pressure rating. A well-selected receiver gives better value by supporting stable pressure and reducing unnecessary compressor workload.
Understanding Air Receiver Tank for Cement Industry Price
The Air Receiver Tank for Cement Industry Price depends on several factors, including capacity, design pressure, shell thickness, material grade, orientation, fittings, coating, inspection requirements, and customisation. Larger-capacity tanks and higher-pressure units generally require more material and fabrication work.
However, price should not be the only consideration. A low-cost tank that does not match the application may lead to operating issues, additional maintenance, or reduced system efficiency. Divya Engineers Private Limited helps clients obtain an Air Receiver Tank for Cement Industry at Best Price by balancing practical performance, reliable construction, and project requirements.
Frequently Asked Questions
An Air Receiver Tank stores compressed air, stabilises pressure, manages peak demand, and supports pneumatic equipment used throughout the cement manufacturing process.
Yes. Capacity, pressure rating, tank orientation, nozzle arrangement, mounting type, and coating can be selected according to the application.
If you are searching for Air Receiver Tank for Cement Industry Near Me, choose a manufacturer that can understand your technical needs, provide clear specifications, and deliver dependable fabrication quality.
Yes. Divya Engineers Private Limited also serves as an Air Receiver Tank for Cement Industry Exporter for customers seeking robust industrial compressed-air storage solutions for international projects.
Request Your Quote Today
A reliable Air Receiver Tank for Cement Industry is a smart investment for maintaining stable compressed-air performance, reducing compressor stress, and supporting uninterrupted cement production. Divya Engineers Private Limited can help you select a tank that suits your pressure, capacity, and installation requirements.
Contact our team today for product specifications, customised options, and a competitive quotation for your cement plant air-storage requirement.
Top of Form
Bottom of Form