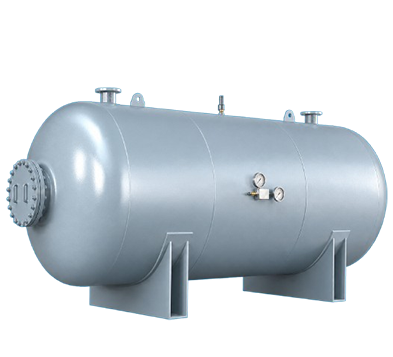
150 Litre Air Receiver Tank – Divya Engineers Private Limited
A reliable compressed-air system needs more than a high-performing compressor. It also needs the right storage solution to maintain steady pressure, manage peak demand, and support cleaner air delivery. A 150 Litre Air Receiver Tank is an ideal choice for small and medium industrial operations that require dependable compressed-air storage without using excessive floor space. Divya Engineers Private Limited provides well-engineered tanks designed for practical performance, long service life, and safer operation.
Whether used with air compressors in workshops, manufacturing units, packaging lines, automotive facilities, or process industries, a properly selected 150 Litre Air Receiver Tank helps improve the efficiency of the entire pneumatic system. It stores compressed air for immediate use, reduces compressor cycling, and assists in separating moisture from the air stream.
What Is a 150 Litre Air Receiver Tank?
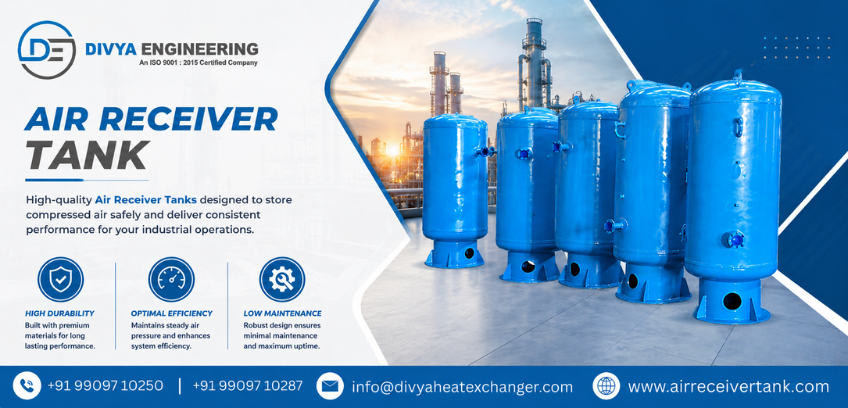
A 150 Litre Air Receiver Tank is a pressure vessel designed to store compressed air generated by an air compressor. It acts as a buffer between the compressor and the application equipment. This stored air can be released quickly when demand rises, helping maintain a stable operating pressure.
An Air Receiver Tank also allows compressed air to cool down. As the air cools, moisture and oil vapours can condense, making it easier to remove them through a drain valve or moisture-management system. This supports better air quality and helps protect pneumatic tools, valves, cylinders, and downstream machinery.
For businesses that need a compact yet useful storage capacity, a 150 Litre Air Receiver Tank provides a balanced solution. It is suitable for intermittent air demand, moderate production requirements, and installations where a larger vessel may not be necessary.
Key Features of a 150 Litre Air Receiver Tank
Divya Engineers Private Limited focuses on practical construction and dependable engineering. Our tanks can be selected according to the required pressure rating, material preference, orientation, and installation condition.
Strong and Durable Construction
The tank body is manufactured using suitable quality material and robust fabrication methods to withstand compressed-air pressure. Proper welding, surface finishing, and structural design help ensure reliability during daily industrial use.
Stable Air Pressure Support
A 150 Litre Air Receiver Tank stores compressed air and releases it when demand increases. This helps reduce sudden pressure drops and supports smoother operation of connected equipment.
Moisture Separation Benefits
As air remains inside the vessel, it cools and allows water vapour to condense. With appropriate drainage arrangements, the tank contributes to moisture control and helps reduce corrosion risks in the compressed-air line.
Compact Capacity for Industrial Use
The 150-litre capacity is suitable for many small and mid-sized facilities. It offers useful air storage while remaining manageable for installation in workshops, service areas, fabrication units, and production floors.
Customisation Options
As a trusted 150 Litre Air Receiver Tank Manufacturer, Divya Engineers Private Limited can support requirements related to pressure ratings, vertical or horizontal configuration, nozzle connections, accessories, and protective coatings, subject to the application needs.
Applications of an Air Receiver Tank
A 150 Litre Air Receiver Tank can serve a wide range of industries where compressed air is required for regular operations. Common applications include:
Automobile service centres and garages
Pneumatic tool operations
Packaging and sealing machines
Small manufacturing units
CNC and fabrication workshops
Printing and labelling equipment
Paint booths and spray applications
Food-processing support systems
Textile and assembly operations
The correct tank capacity depends on compressor output, pressure requirement, air consumption pattern, and peak demand. Choosing the right size helps improve air availability and supports energy-efficient compressor operation.
Quality That Supports Long-Term Performance
Quality is extremely important in every pressure vessel. At Divya Engineers Private Limited, each 150 Litre Air Receiver Tank is developed with attention to material selection, fabrication accuracy, weld quality, fittings, and finishing. A well-made tank should offer structural strength, dependable pressure handling, and convenient access for inspection and drainage.
Regular maintenance is equally important. Operators should inspect the tank, fittings, pressure gauge, safety valve, and drain system at scheduled intervals. Draining accumulated moisture prevents internal corrosion and helps extend the useful life of the vessel. Proper installation on a stable base and operation within the specified pressure limits are essential for safe performance.
Why Choose Divya Engineers Private Limited?
Choosing the right supplier is as important as choosing the correct tank capacity. Divya Engineers Private Limited understands that industrial buyers need products that fit their system, budget, and operational expectations.
As an experienced 150 Litre Air Receiver Tank Supplier, we focus on offering dependable solutions for varied industrial needs. We help customers select suitable specifications based on compressor capacity, working pressure, air usage, and site conditions.
Customers searching for the Best 150 Litre Air Receiver Tank value durability, reliable construction, and clear technical support. Our team works to provide a product that supports efficient compressed-air storage and smooth day-to-day operation. If your business needs a Top 150 Litre Air Receiver Tank for a new installation or system upgrade, we can guide you through the right configuration.
We also serve buyers who need supply support beyond local markets. As a 150 Litre Air Receiver Tank Exporter, Divya Engineers Private Limited can assist with product requirements for different industrial applications and delivery needs.
How to Select the Right Tank
Before you Buy 150 Litre Air Receiver Tank, consider these important points:
Working Pressure
The pressure rating of the vessel must match or exceed the compressor system’s operating pressure. Never choose a tank with an unsuitable pressure rating.
Air Demand Pattern
If your equipment uses air in short, high-demand bursts, the tank helps meet those peaks without placing unnecessary strain on the compressor.
Installation Space
Choose vertical or horizontal orientation according to available floor space, accessibility, and piping layout.
Air Quality Needs
For moisture-sensitive applications, combine the tank with appropriate filters, dryers, and drain arrangements to support clean compressed air.
Cost and Value
The 150 Litre Air Receiver Tank Price depends on design specifications, pressure capacity, material, orientation, accessories, and finishing requirements. Rather than selecting only on initial cost, consider build quality, safety features, and long-term operating value.
Frequently Asked Questions
It stores compressed air, supports stable system pressure, manages peak demand, and helps reduce moisture in the air line.
It can be used with many compressor systems when the capacity and pressure rating are properly matched. Always confirm technical compatibility before installation.
The drain frequency depends on humidity, compressor usage, and air-treatment equipment. In many installations, regular daily or scheduled draining is recommended to prevent water accumulation.
Divya Engineers Private Limited can help businesses identify the right supply option based on their location, specifications, and required delivery schedule.
Get the Right Air Storage Solution Today
If you are looking for a dependable 150 Litre Air Receiver Tank at Best Price, Divya Engineers Private Limited is ready to help. Share your compressor capacity, operating pressure, application, and installation requirement with our team. We will assist you in selecting a safe, durable, and efficient air receiver solution for your operation.
Contact Divya Engineers Private Limited today to discuss your requirement and receive professional support for a high-quality compressed-air storage system.