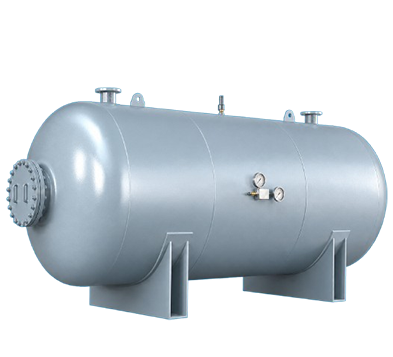
100 Litre Air Receiver Tank – Divya Engineers Private Limited
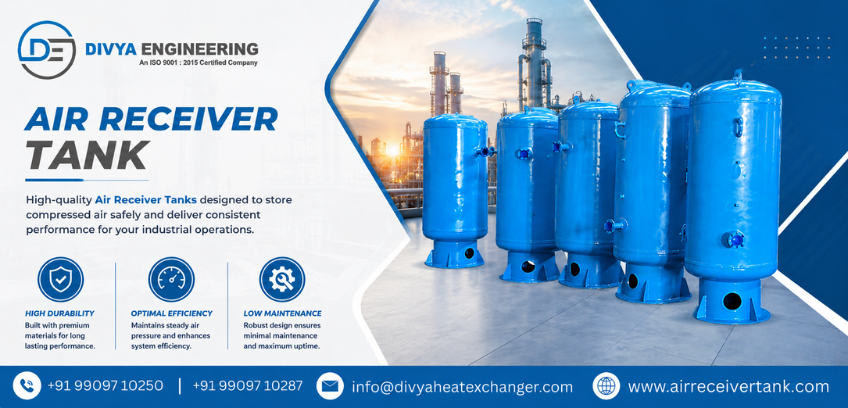
A dependable 100 Litre Air Receiver Tank is an essential part of a compressed-air system. It stores compressed air, helps maintain stable pressure, reduces frequent compressor cycling, and supports smoother equipment performance. Divya Engineers Private Limited designs and supplies robust tanks for workshops, manufacturing units, garages, packaging lines, and other industrial applications where a compact yet reliable air-storage solution is needed.
Choosing the right 100 Litre Air Receiver Tank is not only about capacity. The tank must suit your operating pressure, air demand, available installation space, and safety requirements. With careful engineering, quality materials, and practical customization options, Divya Engineers Private Limited helps businesses improve the efficiency and dependability of their compressed-air setup.
Why a 100 Litre Air Receiver Tank Matters
An Air Receiver Tank acts as a storage buffer between the compressor and the points of use. It holds compressed air so that short-term demand peaks can be handled without an immediate pressure drop. This improves the consistency of pneumatic tools, automation equipment, spray-painting systems, and production machinery.
A properly sized 100 Litre Air Receiver Tank can also reduce compressor start-stop cycles. Fewer cycles can support better energy management and lower wear on the compressor. For small and medium-scale operations, 100 litres is often a practical capacity that balances storage performance with limited floor space.
Key Features of a 100 Litre Air Receiver Tank
Divya Engineers Private Limited focuses on tanks that are built for dependable industrial use. Our 100 Litre Air Receiver Tank solutions can be configured according to required pressure ratings, connection sizes, orientation, and site conditions.
Key features include:
Strong, durable construction for regular compressed-air storage
Designed for stable pressure delivery and efficient air buffering
Suitable for vertical or horizontal installation, depending on space
Provision for inlet, outlet, drain, pressure gauge, and safety valve connections
Interior and exterior finishing options based on application needs
Easy access for periodic drainage and maintenance
Compact capacity suitable for workshops and industrial utility systems
The design of an Air Receiver Tank should always consider safety and serviceability. Proper draining is particularly important because moisture may condense inside the tank. Regular removal of condensate helps protect downstream equipment and improves air quality.
Applications Across Industries
A 100 Litre Air Receiver Tank is widely used wherever compressed air is required in a controlled and consistent manner. It is useful for pneumatic tools, CNC support systems, tyre inflating stations, dust-cleaning systems, printing units, packaging machinery, fabrication shops, and small production lines.
It can also support air-drying and filtration arrangements by allowing the air to cool before it reaches downstream equipment. This may help separate moisture more effectively when paired with suitable filters and drains. Whether the application requires intermittent bursts of air or a steady flow, the right tank configuration can make a noticeable difference.
Businesses searching for a 100 Litre Air Receiver Tank Manufacturer should look beyond capacity alone. Material selection, weld quality, pressure compatibility, inspection practices, and after-sales support are equally important factors.
Quality You Can Rely On
At Divya Engineers Private Limited, quality is considered at every stage of tank manufacturing. From raw-material selection and fabrication to welding, finishing, and final checks, our process is focused on delivering consistent performance and long service life.
As a trusted 100 Litre Air Receiver Tank Supplier, we understand that industrial buyers need equipment that can integrate smoothly with their existing compressor systems. Tanks are produced with attention to dimensional accuracy, sound fabrication practices, leak prevention, and suitable connection arrangements.
The right 100 Litre Air Receiver Tank should be selected according to the compressor’s output, operating pressure, duty cycle, and consumption pattern. Our team can help you identify a suitable solution for your specific application instead of offering a one-size-fits-all product.
Why Choose Divya Engineers Private Limited?
Divya Engineers Private Limited combines practical engineering knowledge with a customer-focused approach. We aim to make the selection and supply process simple, transparent, and dependable for every client.
Our advantages
Application-based guidance for selecting the right tank
Reliable manufacturing standards and durable fabrication
Options for customized pressure ratings and fittings
Timely supply for industrial and commercial requirements
Support for domestic as well as overseas requirements
Focus on safety, performance, and long-term value
If you require a dependable 100 Litre Air Receiver Tank Exporter, our team can support packaging, documentation, and supply requirements for international customers. We work to ensure that each order is handled with care from enquiry through dispatch.
How to Select the Right Tank
Before you Buy 100 Litre Air Receiver Tank, review the working pressure of your compressor, expected air consumption, available area, and connection requirements. A vertical tank is often preferred where floor space is limited, while a horizontal design may suit installations with specific layout needs.
It is also wise to ask about drainage arrangements, corrosion protection, inspection provisions, and compatible safety accessories. When comparing the 100 Litre Air Receiver Tank Price, focus on overall value rather than only the initial purchase cost. A well-built tank can provide safer, more stable, and more economical service over time.
Customers looking for the Best 100 Litre Air Receiver Tank should choose a product that matches their application and is backed by knowledgeable technical support. Divya Engineers Private Limited helps customers make that decision with confidence.
Frequently Asked Questions
A 100 Litre Air Receiver Tank stores compressed air and stabilizes pressure in the air system. It helps manage short demand peaks and reduces unnecessary compressor cycling.
Pricing depends on factors such as material grade, design pressure, tank orientation, fittings, coatings, testing requirements, and customization needs.
Yes. It is often a suitable choice for small workshops, garages, service centres, and medium-duty pneumatic applications. The final choice should be based on actual air demand and compressor output.
Divya Engineers Private Limited supplies tanks for customers across industrial locations. Contact our team with your city and technical requirement to check availability and delivery options.
Get a Reliable Tank for Your Air System
When you need a Top 100 Litre Air Receiver Tank that delivers reliable storage, stable pressure, and durable performance, Divya Engineers Private Limited is ready to assist. We offer practical guidance, dependable manufacturing, and responsive service for diverse compressed-air applications.
Contact us today to request specifications, discuss customization, and get a quote for a 100 Litre Air Receiver Tank at Best Price. Choose Divya Engineers Private Limited for a safe, efficient, and long-lasting compressed-air storage solution.