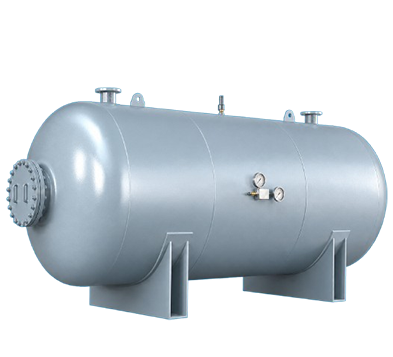
100 Litre Air Receiver Tank Supplier – Divya Engineers Private Limited
Compressed air plays an important role in workshops, manufacturing units, engineering plants, pneumatic systems, and many other industrial applications. A properly selected 100 Litre Air Receiver Tank Supplier can help businesses maintain stable air pressure, manage short-term demand variations, and improve the overall performance of their compressed-air system. Divya Engineers Private Limited manufactures and supplies industrial air receivers designed with attention to construction quality, application requirements, and dependable service.
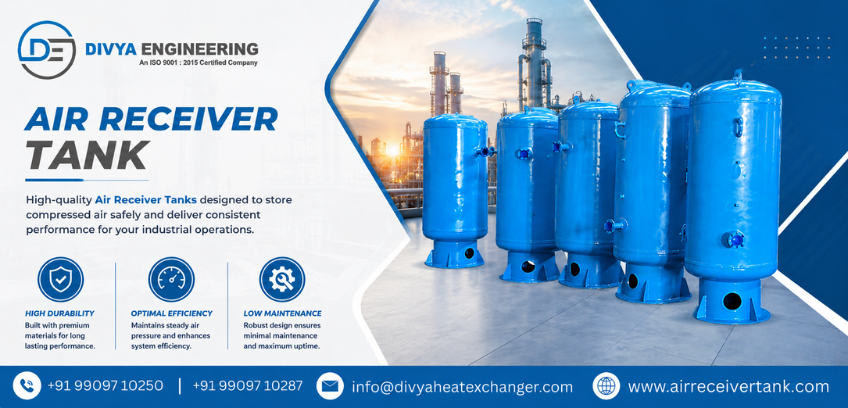
A 100-litre receiver is a practical storage option for applications where a compact compressed-air buffer is required. An Air Receiver Tank stores compressed air between the compressor and the point of use. This stored air can support peak demand, reduce pressure fluctuations, and minimize unnecessary compressor cycling. Receiver tanks are available in different materials, pressure ratings, orientations, and configurations, so the exact specification should always be selected according to the application.
Why Choose a 100 Litre Air Receiver Tank Supplier?
A 100-litre tank can be useful where space is limited but a compressed-air storage buffer is still required. It can support pneumatic tools, small production equipment, workshops, automation systems, air-operated machinery, and other applications.
The primary functions of a receiver include:
Storing compressed air for temporary demand
Helping stabilize system pressure
Reducing frequent compressor starts and stops
Supporting compressor efficiency
Providing a buffer during short demand peaks
Helping separate moisture from compressed air
Supporting smoother pneumatic equipment operation
The correct tank capacity depends on compressor output, operating pressure, air consumption, duty cycle, and the characteristics of the application. Therefore, purchasing a tank based only on capacity is not recommended.
Features of a Quality Air Receiver Tank
A dependable receiver should combine strong construction, appropriate pressure capability, good fabrication, and suitable accessories. Industrial manufacturers commonly offer vertical and horizontal designs, with specifications selected according to the customer's requirements.
Robust Construction
The tank should be manufactured from suitable pressure-vessel material with properly controlled fabrication and welding. Strong construction supports reliable operation over an extended service period.
Suitable Pressure Rating
Working and design pressure must be selected according to the compressed-air system. The receiver should never be operated beyond its approved pressure limits.
Efficient Space Utilization
A 100-litre receiver can provide useful air storage without requiring the footprint of a much larger vessel. Vertical designs can be particularly useful where floor space is restricted.
Safety Components
Depending on the design and application, receiver systems can incorporate pressure gauges, safety relief valves, drain valves, and suitable inlet and outlet connections.
Corrosion Protection
Compressed air can contain moisture, which may contribute to internal corrosion. Proper condensate drainage and suitable external protection can help improve service life.
Best 100 Litre Air Receiver Tank Supplier for Industrial Applications
The Best 100 Litre Air Receiver Tank Supplier should understand that different customers have different operating conditions. A workshop using pneumatic tools may have different requirements from an automated production line or a specialized industrial process.
Divya Engineers Private Limited focuses on application-oriented manufacturing and supplies air receivers for industrial compressed-air systems. The company's product range includes air receivers and other pressure equipment, with a focus on quality materials and national and international quality requirements.
Before selecting a tank, customers should discuss compressor capacity, required pressure, installation position, connection sizes, material preferences, and applicable design requirements with the manufacturer.
Top 100 Litre Air Receiver Tank Supplier – What Quality Means
A Top 100 Litre Air Receiver Tank Supplier should offer more than a competitive quotation. Product quality begins with suitable raw materials and continues through fabrication, welding, inspection, finishing, and final testing.
Important quality considerations include:
Appropriate pressure-vessel-grade material
Accurate dimensions
Consistent welding quality
Properly finished connections
Suitable pressure testing
Quality inspection documentation where required
Protective surface treatment
Secure packaging and transportation
Quality control is particularly important because an air receiver is a pressurized vessel. Customers should always select a product manufactured for the intended operating conditions rather than choosing solely on the lowest initial price.
100 Litre Air Receiver Tank Manufacturer with Application-Focused Solutions
As a 100 Litre Air Receiver Tank Manufacturer, Divya Engineers Private Limited can support customers looking for compact compressed-air storage equipment for different industrial applications. The company emphasizes engineering, material quality, fabrication, and application suitability.
A receiver can be supplied according to the required configuration, subject to technical feasibility and project specifications. Depending on the application, customers may require different materials, mounting arrangements, pressure ratings, connections, or surface finishes.
100 Litre Air Receiver Tank Price – What Determines the Cost?
The 100 Litre Air Receiver Tank Price is influenced by several factors rather than capacity alone. Material selection, working pressure, design requirements, tank orientation, accessories, coating, inspection, customization, and quantity can affect the final quotation.
Customers searching for an affordable solution should compare overall value. A low-cost tank may not provide the required specification, while a properly engineered receiver can offer better reliability and long-term value.
For an accurate quotation, provide the supplier with your required capacity, pressure rating, material, orientation, application, and delivery location.
100 Litre Air Receiver Tank Exporter for Domestic and Global Requirements
Businesses purchasing pressure equipment for projects outside their local market can work with an experienced 100 Litre Air Receiver Tank Exporter. Export supply may require appropriate documentation, packaging, shipping coordination, and technical specifications based on the destination market.
Divya Engineers Private Limited serves industrial customers and provides pressure equipment solutions for domestic and suitable international requirements. Its Ahmedabad-based operation manufactures air receivers and related pressure equipment.
Top Cities of India We Serve
Divya Engineers Private Limited can cater to industrial requirements across major Indian manufacturing and commercial centers, including:
Ahmedabad, Vadodara, Surat, Rajkot, Bharuch, Ankleshwar, Vapi, Mumbai, Pune, Nashik, Nagpur, Delhi, Gurugram, Noida, Ghaziabad, Faridabad, Jaipur, Indore, Bhopal, Hyderabad, Bengaluru, Chennai, Coimbatore, Hosur, Kolkata, Visakhapatnam, Bhubaneswar, Raipur, Ranchi, Patna, Lucknow, Chandigarh, and Mohali.
For customers searching for a 100 Litre Air Receiver Tank Supplier Near Me, proximity can be useful, but product quality, technical suitability, delivery capability, and after-sales support should also be considered.
Frequently Asked Questions
It is a compressed-air storage vessel with a nominal capacity of 100 litres. It provides a buffer of stored air between the compressor and the point of consumption.
It can be used with suitable small and medium compressed-air applications, including pneumatic tools, workshops, automation equipment, and production machinery.
Depending on project requirements, manufacturers may provide variations in material, orientation, pressure rating, connections, supports, and other specifications.
Share your required pressure, application, material preference, orientation, quantity, and delivery location with Divya Engineers Private Limited. The technical team can help determine a suitable configuration and provide a quotation.
Regularly inspect the vessel, fittings, pressure-related components, and supports. Condensate should also be drained according to the operating environment and manufacturer's recommendations. Required inspections and safety procedures should follow applicable regulations.
Divya Engineers Private Limited combines manufacturing experience with an application-focused approach to industrial pressure equipment. The company offers air receivers designed for dependable compressed-air storage, with emphasis on quality materials, fabrication, inspection, and customer requirements. Its established product portfolio includes air receivers, nitrogen tanks, chemical tanks, liquid tanks, heat exchangers, and related industrial equipment.
If you are planning to purchase a 100-litre receiver for a workshop, manufacturing unit, pneumatic system, or industrial project, choosing the right supplier can make a significant difference.
Contact Divya Engineers Private Limited today with your required pressure, application, material, quantity, and delivery location. Get expert guidance and a competitive quotation for a reliable 100-litre compressed-air storage solution tailored to your requirements.