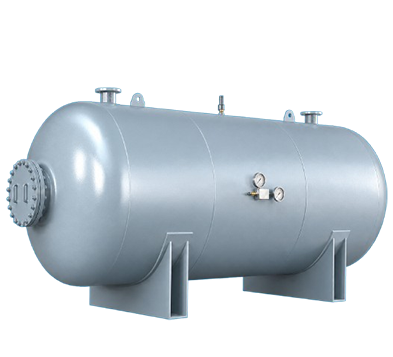
100 Litre Air Receiver Tank Exporter – Divya Engineers Private Limited
A reliable compressed-air system needs more than a compressor. It also needs safe and stable air storage to manage pressure fluctuations, reduce compressor cycling, and support smooth production. Divya Engineers Private Limited is a trusted 100 Litre Air Receiver Tank Exporter offering robust, precision-engineered tanks for industrial clients across global markets. Our 100-litre tanks are designed for dependable performance in workshops, manufacturing plants, automation lines, pneumatic tools, and small-to-medium compressed-air applications.
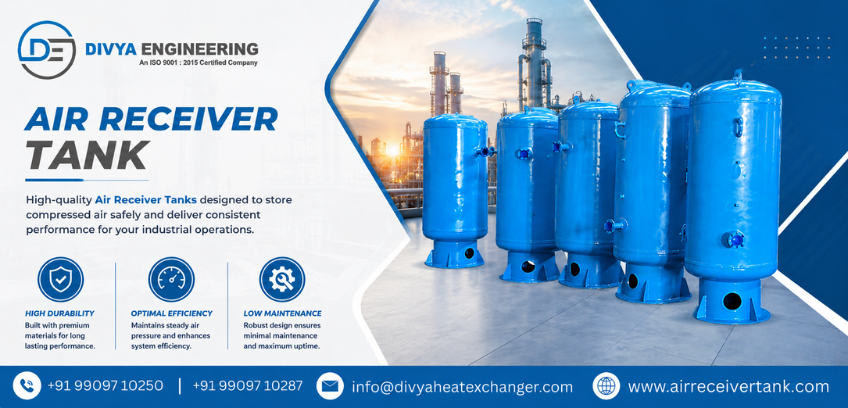
A properly selected Air Receiver Tank stores compressed air and releases it when demand suddenly rises. This helps maintain consistent pressure, improves equipment efficiency, and supports cleaner, more controlled operations. As an experienced Air Receiver Tank Exporter, we focus on quality materials, dependable fabrication, secure packing, and responsive support for international buyers.
Why Choose a 100-Litre Air Receiver Tank?
A 100-litre capacity is a practical choice where moderate compressed-air storage is required without using excessive floor space. It is well suited to systems using pneumatic machines, spray-painting equipment, packaging units, garages, fabrication shops, CNC support applications, and assembly operations.
A 100 Litre Air Receiver Tank Exporter understands that every plant has different pressure, airflow, and installation requirements. The right tank creates a buffer between the compressor and end-use equipment. It allows the compressor to run more efficiently, reduces pressure drops during peak demand, and helps limit frequent start-stop cycles.
The tank may also assist in cooling compressed air, allowing some moisture to condense before it travels further through the air line. When combined with suitable drains, filters, dryers, and pressure-control accessories, it contributes to a more reliable compressed-air setup.
Key Features of Our 100-Litre Tanks
At Divya Engineers Private Limited, each 100 Litre Air Receiver Tank Exporter solution is developed with practical industrial use in mind. Depending on the application, customers can discuss suitable material grade, pressure rating, orientation, nozzles, connection sizes, coating, and documentation requirements.
Strong and Functional Construction
Our tanks are fabricated using quality-approved raw materials and sound manufacturing practices. We offer options suitable for different operating environments, including mild-steel and stainless-steel configurations where required. Properly designed shell thickness, heads, weld joints, and support arrangements help achieve stable long-term service.
Useful Design Options
A 100-litre tank can be supplied in vertical or horizontal form depending on available space and drainage needs. Vertical tanks are often preferred when floor area is limited, while horizontal tanks may suit specific layout requirements. We can provide required inlet, outlet, pressure-gauge, safety-valve, drain, and inspection connections based on your system design.
Better Air Availability
By storing compressed air close to the point of use, a tank can handle short bursts of demand more effectively. This improves operating stability for pneumatic tools and equipment. If you plan to Buy 100 Litre Air Receiver Tank units for a production line, correct capacity and pressure matching are essential for dependable results.
Quality Assurance for Export-Ready Supply
Quality is central to every 100 Litre Air Receiver Tank Exporter order handled by Divya Engineers Private Limited. Pressure vessels must be manufactured and inspected carefully because they operate under compressed-air pressure. Our quality process includes material checks, dimensional verification, controlled fabrication, welding inspection, and pressure testing as per agreed project requirements.
We pay close attention to weld quality, nozzle alignment, surface preparation, coating, and leakage prevention. Hydrostatic testing may be carried out where specified, and relevant test records can be provided according to the order scope. Export packing is planned to protect the tank from handling damage, moisture, and transit-related risks.
As a dependable 100 Litre Air Receiver Tank Manufacturer, we also guide buyers on technical details such as working pressure, test pressure, installation orientation, operating temperature, and accessory requirements. This helps buyers receive a tank that fits their compressor system instead of choosing only on capacity or cost.
Why Divya Engineers Private Limited?
Choosing the Best 100 Litre Air Receiver Tank Exporter means choosing a supplier that understands both product performance and export coordination. We work with buyers who need consistent quality, clear communication, and application-focused solutions.
Key reasons to choose us include:
Reliable fabrication for industrial compressed-air applications
Customised pressure ratings, nozzles, sizes, and finishes
Support for vertical and horizontal receiver tank designs
Quality checks and test documentation as required
Export-oriented packing and dispatch coordination
Timely response for bulk, repeat, and project-based requirements
As a 100 Litre Air Receiver Tank Supplier, we aim to build long-term partnerships through honest technical assistance and dependable product supply. We do not believe that one design fits every requirement; we discuss the operating conditions before suggesting the suitable receiver-tank specification.
Understanding 100 Litre Air Receiver Tank Price
The 100 Litre Air Receiver Tank Price depends on several factors, including material grade, working pressure, shell thickness, orientation, fittings, surface coating, testing requirements, certification, order quantity, packing, and export destination. A lower initial price may not always offer the same safety, durability, or documentation support.
When comparing quotations, check the complete technical scope. Confirm the tank’s capacity, design pressure, test pressure, material, accessories, mounting arrangement, paint system, and delivery terms. This approach helps you compare value accurately and avoid unexpected changes later.
Industries and Applications We Serve
A Top 100 Litre Air Receiver Tank Exporter supplies products that can support many industries, including:
Automobile workshops and service centres
Engineering and fabrication units
Packaging and printing operations
Food-processing and dairy plants
Pharmaceutical and chemical facilities
Textile and plastic machinery
Pneumatic-tool and automation systems
Paint shops and powder-coating lines
For demanding applications, the system should be designed by qualified personnel. Correct installation, pressure relief protection, periodic inspection, and moisture drainage are important for safe operation.
Top Cities of India We Serve
Divya Engineers Private Limited supplies and supports customers in leading industrial locations across India, including Ahmedabad, Vadodara, Surat, Rajkot, Vapi, Ankleshwar, Mumbai, Pune, Nashik, Nagpur, Bengaluru, Chennai, Hyderabad, Coimbatore, Delhi, Noida, Gurugram, Faridabad, Jaipur, Kolkata, Visakhapatnam, Indore, Bhopal, Ludhiana, Chandigarh, Kochi, and Bhubaneswar.
If you are searching online for a 100 Litre Air Receiver Tank Exporter Near Me, our team can help you identify the right technical configuration and arrange supply based on your location and project needs.
Frequently Asked Questions
It stores compressed air, manages short-term demand changes, helps stabilise system pressure, and can reduce compressor cycling.
Select it according to the compressor’s operating pressure and your system’s design requirements. Always consider a suitable safety margin and consult a qualified technical team.
Yes. As a professional Air Receiver Tank, export and manufacturing partner, we can discuss custom connections, pressure ratings, mounting, orientation, materials, and coating requirements.
Both can work well. Vertical tanks save floor space and support drainage, while horizontal tanks can suit particular equipment layouts.
Documentation and testing records can be provided as per the agreed order scope, destination requirements, and applicable specifications.
Contact Divya Engineers Private Limited Today
For a dependable 100 Litre Air Receiver Tank Exporter, choose Divya Engineers Private Limited. Share your capacity, pressure, material, application, and destination requirements with our team. We will help you select a reliable tank built for safe performance and efficient compressed-air storage. Contact us today for a customised quotation and professional export support.